Manufacturing
Connect the Plant. Run on Real-Time Data.
We help discrete, process and contract manufacturers connect shop-floor, quality, maintenance and enterprise systems. Production is visible as it happens, quality is traceable, and AI goes where it prevents downtime, with engineers making the final call.
Most plants already have the data. It’s stuck in machines, spreadsheets and systems that don’t talk. Smart manufacturing starts with connecting what you run today, not with buying a new factory.
25%India’s target share of GDP from manufacturing
11%of revenue large manufacturers lose to unplanned downtime
Manufacturing Now
India Is Scaling Manufacturing. Plants Must Get Smarter.
Policy support, new capacity and rising cost pressure are changing how manufacturers plan, produce and compete.
- ₹1.76 Lakh Cr
investment attracted under the PLI scheme across 14 sectors
New capacity needs connected systems from day one.
Source: Government of India, Press Information Bureau, Aug 2025
- ₹16.5 Lakh Cr
sales by PLI beneficiaries so far
Higher output raises the bar for quality, traceability and uptime.
Source: Government of India, Press Information Bureau, Aug 2025
- 11%
of revenue lost to unplanned downtime at the world’s 500 largest companies
Up from 8% in 2019. Every hour of stoppage costs more than before.
- $1.4T
lost each year to unplanned downtime by those same companies
Predictable uptime is now a competitive edge.
Strategic Priorities
The Problems Manufacturing Leaders Bring to Us
Six recurring issues we hear from plant, operations, quality and technology leaders. Each one maps to the capabilities further down this page.
- P01
No Real-Time Shop-Floor Visibility
Production status is collected by hand at the end of a shift.
We often hear“We see yesterday’s problems today.”
- P02
Disconnected IT and OT
Machines, MES, SCADA and ERP run as separate worlds.
We often hear“The ERP doesn’t know what the line actually made.”
- P03
Unplanned Downtime
Equipment fails without warning, and maintenance is reactive.
We often hear“We fix machines after they stop.”
- P04
Quality Found Too Late
Defects are caught at final inspection, not at the source.
We often hear“By the time we spot the defect, the batch is done.”
- P05
Paper-Based Operations
Work instructions, checklists and logs are still on paper.
We often hear“Our audit trail is a filing cabinet.”
- P06
Planning That Can’t Keep Up
Production plans don’t adjust to demand, material or capacity changes.
We often hear“Every schedule change means a day of spreadsheets.”
Segments
Who We Work With in Manufacturing
Each type of plant produces, measures and is regulated differently. We shape the work to fit.
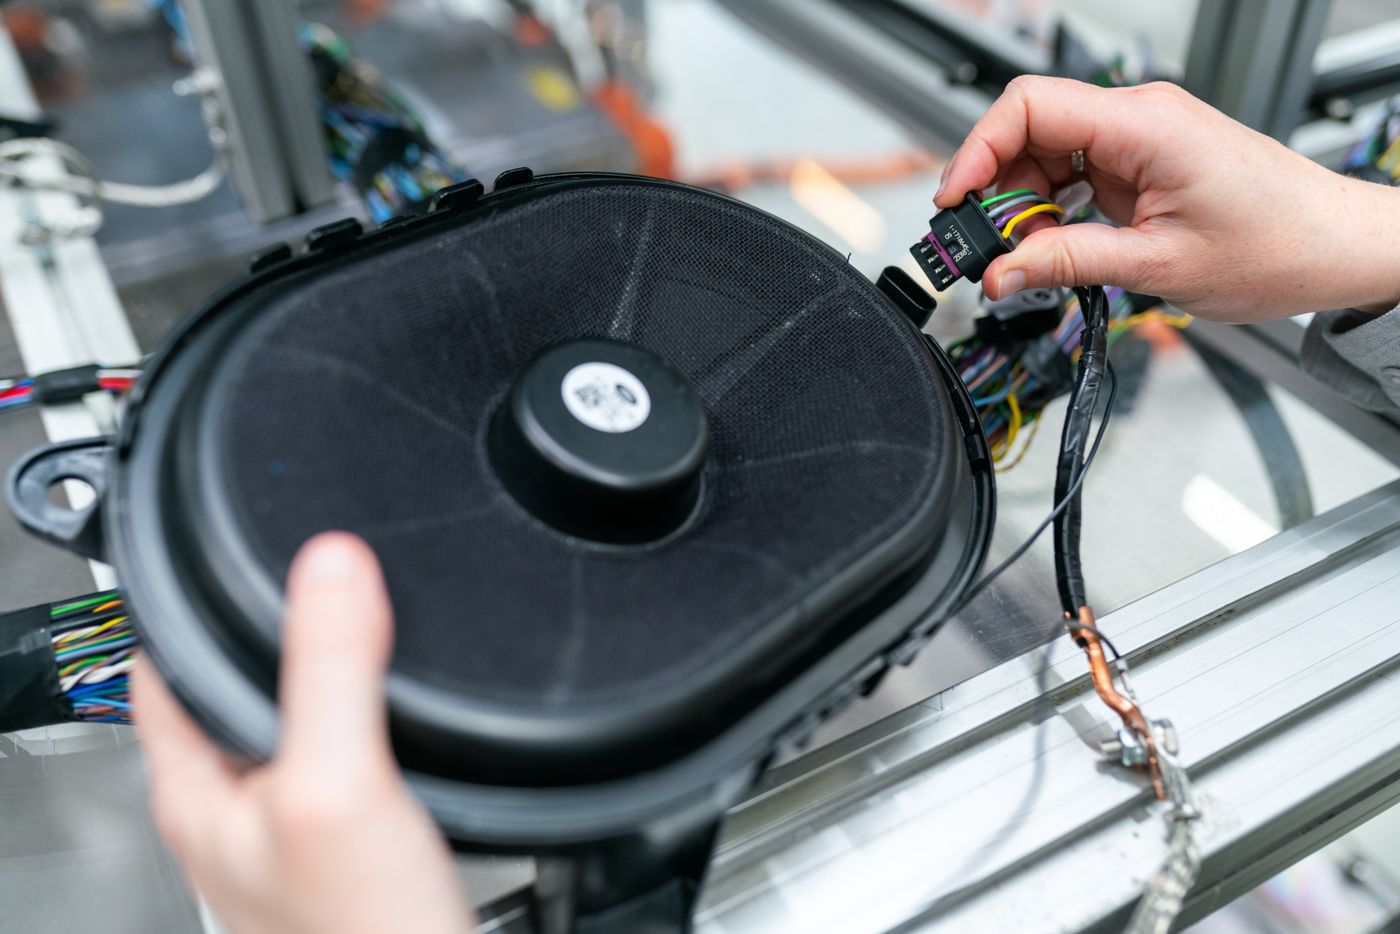
Discrete Manufacturing
Automotive, auto components, industrial equipment, electronics
Connect lines, machines and ERP for live output, OEE and traceability.
- Plant Head
- Manufacturing IT
- Production Manager
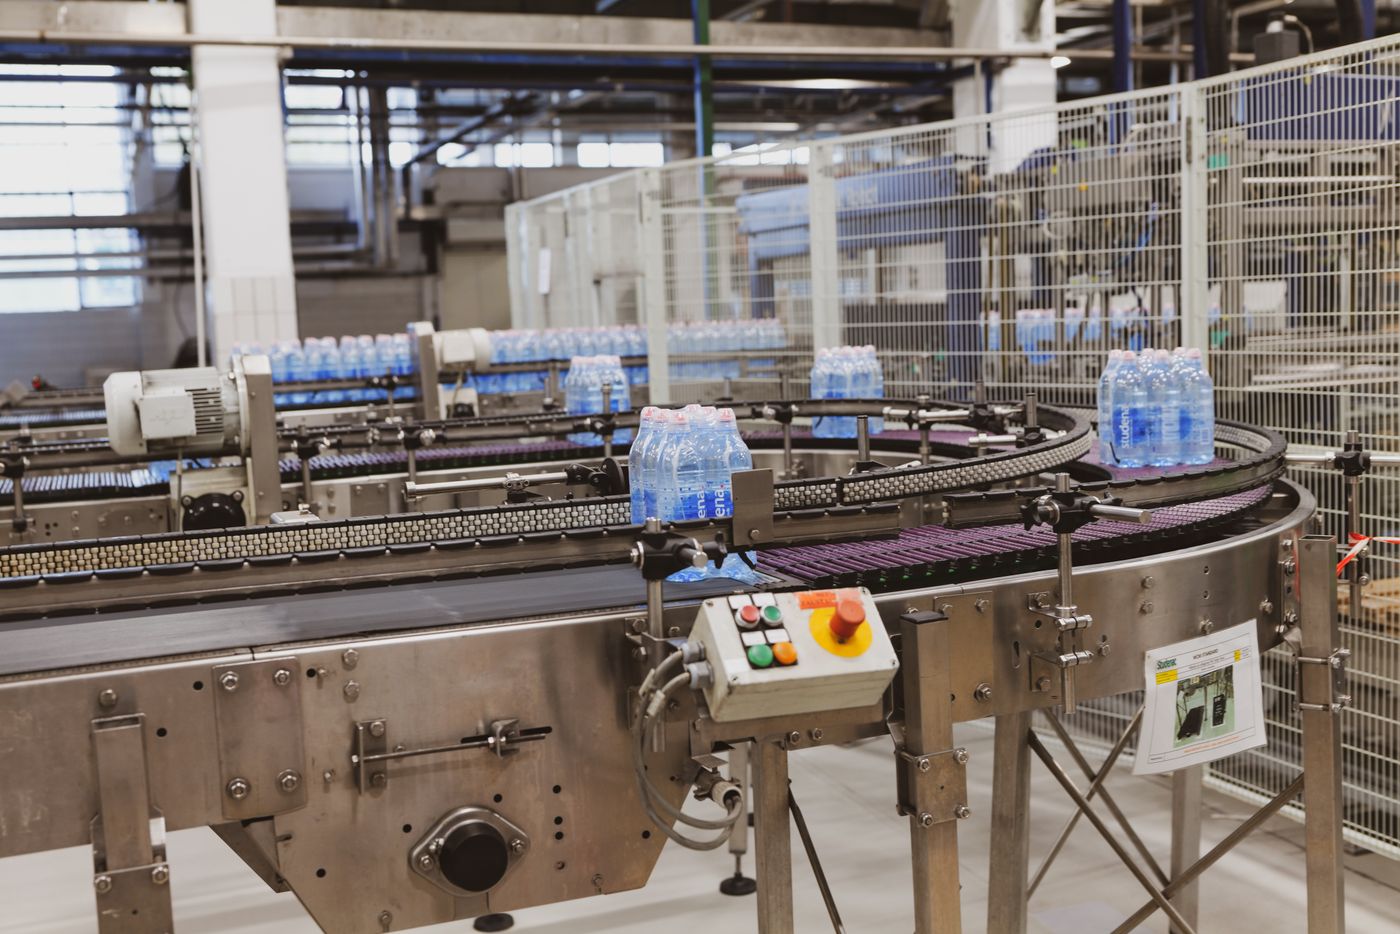
Process Manufacturing
Chemicals, FMCG, food & beverage, pharma
Digitise batches, quality checks and process data for consistency and compliance.
- Operations Head
- Quality Head
- Process Engineering
Contract Manufacturers & EMS
Contract manufacturing, electronics manufacturing services
Run multi-customer production with clear traceability and reporting.
- COO
- Programme Manager
- IT Director
Industrial & Engineering Firms
Heavy engineering, capital goods, fabrication
Connect projects, production, assets and service for complex, made-to-order work.
- CEO
- Engineering Head
- After-Sales Service
Value Chain & Use Cases
Where We Help Across the Manufacturing Value Chain
Use cases we deliver at each stage, tagged by the capability behind them.
Design & Engineering
- PLM and ERP integration for product dataIntegration
- Engineering document search and change trackingAI
Plan
- Production planning and scheduling dashboardsData
- Demand and material forecastingAI
Produce
- Machine connectivity (IIoT) and live OEE dashboardsData
- MES, SCADA and ERP integrationIntegration
Quality
- Digital checklists, deviations and CAPA workflowsAutomation
- Vision-based defect detectionAI
Maintain
- Predictive maintenance from sensor dataAI
- CMMS work orders and spares workflowsAutomation
Ship & Serve
- Batch and serial traceabilityData
- Dealer and field service portalsEngineering
Sample Engagements
What Working With Us Could Look Like
Typical projects based on the problems above, with what we would measure.
 Illustrative engagement
Discrete
Live OEE and Shop-Floor Visibility
- Situation
- Output, downtime and scrap are logged by hand each shift, so problems surface a day late.
- What we would do
- Connect machines and MES to a data platform, and build live OEE and downtime dashboards with reason codes and shift-wise alerts.
- HigherOEE (target)
- Fasterresponse to stoppages
Capabilities
Capabilities Mapped to Your Priorities
See which of our practices answers each priority, so you know where to start.
Application Engineering
Operator apps, portals, APIs
- No Real-Time Shop-Floor Visibility: not a main fit
- Disconnected IT and OT: not a main fit
- Unplanned Downtime: not a main fit
- Quality Found Too Late: not a main fit
- Paper-Based Operations: primary fit
- Planning That Can’t Keep Up: not a main fit
AI & Intelligent Automation
Predictive maintenance, vision, forecasting
- No Real-Time Shop-Floor Visibility: not a main fit
- Disconnected IT and OT: not a main fit
- Unplanned Downtime: primary fit
- Quality Found Too Late: primary fit
- Paper-Based Operations: not a main fit
- Planning That Can’t Keep Up: supporting
Data Engineering & Analytics
IIoT data, OEE, traceability
- No Real-Time Shop-Floor Visibility: primary fit
- Disconnected IT and OT: supporting
- Unplanned Downtime: supporting
- Quality Found Too Late: supporting
- Paper-Based Operations: not a main fit
- Planning That Can’t Keep Up: primary fit
Integration & Workflow Automation
MES, SCADA, ERP, CMMS, PLM
- No Real-Time Shop-Floor Visibility: supporting
- Disconnected IT and OT: primary fit
- Unplanned Downtime: supporting
- Quality Found Too Late: not a main fit
- Paper-Based Operations: supporting
- Planning That Can’t Keep Up: supporting
Cloud, DevOps & Platforms
Edge-to-cloud, scalable, monitored
- No Real-Time Shop-Floor Visibility: supporting
- Disconnected IT and OT: supporting
- Unplanned Downtime: not a main fit
- Quality Found Too Late: not a main fit
- Paper-Based Operations: not a main fit
- Planning That Can’t Keep Up: not a main fit
Secure & Governed Design
OT security, access control, audit trails
- No Real-Time Shop-Floor Visibility: not a main fit
- Disconnected IT and OT: supporting
- Unplanned Downtime: not a main fit
- Quality Found Too Late: supporting
- Paper-Based Operations: supporting
- Planning That Can’t Keep Up: not a main fit
- P01 No Real-Time Shop-Floor Visibility
- P02 Disconnected IT and OT
- P03 Unplanned Downtime
- P04 Quality Found Too Late
- P05 Paper-Based Operations
- P06 Planning That Can’t Keep Up
How We Work
Five Steps From Challenge to Measurable Result
Plant changes are scheduled around production windows and follow your safety and change-control procedures.
Discover the Challenge
Walk the floor and map machines, systems, data, people and where losses happen.
Define Scope & Measures
Agree use cases, deliverables, baselines and the metrics that matter, such as OEE, downtime, scrap and first-pass yield.
Design With Controls
Plan architecture, IT/OT integration, OT security, access controls and human review.
Build & Test
Develop the solution and test it on a pilot line or asset against agreed acceptance criteria.
Roll Out & Improve
Scale line by line and plant by plant, monitor results and keep improving.
Engagement Models
Flexible Ways to Work Together
Choose the model that fits your team, timeline and budget, and change it as your needs grow.
Dedicated Resource Model
Skilled professionals for your teams
Contract Staffing
Flexible hiring for short or long-term needs
Project Delivery
End-to-end execution with defined outcomes
Managed Support
Ongoing support and team augmentation
Technology Consultation
Expert guidance to shape your technology approach
Long-Term Partnership
A strategic partner for your growth journey
FAQs
Questions Manufacturing Teams Ask Us
Talk to us about your plants, systems and goals.
Talk to UsCan TECHAIVV connect our machines, MES and ERP?
Yes, through industrial protocols (such as OPC UA and MQTT), APIs and middleware. What’s possible depends on machine age, controllers, network setup, access permissions and your OT security policies.
Do we need new machines to become a smart factory?
No. Older machines can often be connected with sensors and edge devices. We recommend new equipment only when existing assets truly limit the result.
How do you keep plant systems secure when connecting IT and OT?
We design for network separation, least-privilege access, monitoring and secure data flows, aligned with standards such as ISA/IEC 62443 and your own policies. Security is agreed with your plant and IT teams up front.
Will AI and predictive maintenance work on our data?
It depends on data history, sensor coverage and failure patterns. We start with a pilot on critical assets, measure it against a baseline, and scale only what proves useful.
How do we get started?
With a short discovery of your plants, systems and priorities. Then we agree one use case on one line or asset, plus its measures, and deliver that first.
Let’s Build Together
Build a Plant That Runs on Real-Time Data
Connect your machines and systems, see production as it happens, and put AI where it prevents downtime and defects.
Talk to Us- Connected Shop Floor
- Live Production Data
- Predictive Maintenance
- Traceable Quality